Opal Expands Carton Manufacturing with $70 Million Moorebank Facility
Opal has opened a $70 million folding carton plant in Moorebank, enhancing local production with high-speed printing and advanced waste reduction technology.
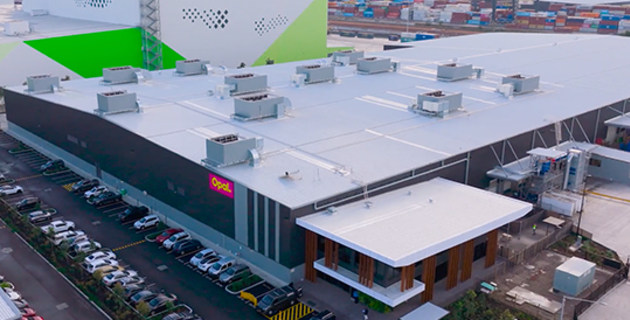
Opal has inaugurated a $70 million purpose-built folding carton manufacturing facility in Moorebank, south-west Sydney, aimed at increasing production efficiency and supporting domestic packaging supply.
Quick Skim
Facility Features Advanced Printing and Waste Reduction Technologies
The Moorebank Cartons site spans 27,233 square metres and houses Australia’s only Heidelberg Boardmaster, a high-speed inline flexographic web printing system designed specifically for folding carton production. This system operates at speeds of up to 600 metres per minute, utilising automated press settings and AI-powered plate scanning to minimise manual adjustments and expedite speed-to-market.
Significantly, the facility integrates advanced changeover technology that reduces board waste during production changeovers to less than 10 metres, representing up to a 90 per cent reduction. This capability is particularly valuable across schedules with multiple packaging formats, enabling better material use and cost efficiency.
Sustainability and Supply Chain Improvements
The site incorporates several sustainability measures, including optimisation for water-based inks to enhance recyclability, energy-efficient drying systems, and heat recovery. Additionally, Moorebank operates without natural gas and consumes less electricity than Opal’s previous facility, improving its environmental footprint.
To streamline supply chains, Opal plans to transport approximately 1557 20-foot containers of board by rail in 2027, utilising connections between the Moorebank Intermodal Precinct and Port Botany, reducing reliance on road freight.
Implications for Packaging Production and Local Supply
According to Brad Hinds, chief executive of packaging at Opal, the investment enables the company to meet evolving customer requirements with greater flexibility and quicker response times. The facility, certified for food-grade manufacturing, supports high-quality, recyclable packaging production domestically, which is critical for Australian food and beverage manufacturers seeking reliable supply and packaging innovation.
The new factory complements Opal’s Centre of Excellence at Orchard Hills, NSW, which focuses on recyclable punnet production, strengthening Opal’s end-to-end packaging development and commercialisation capabilities.
Opal’s Moorebank investment underlines the role of advanced manufacturing technology in sustaining the competitiveness of Australia’s packaging sector, reducing material waste, improving supply chain logistics, and supporting the transition towards more sustainable fibre-based packaging solutions.